How to Fix Drill Press Wobble: Setup, Checks, and Common Mistakes
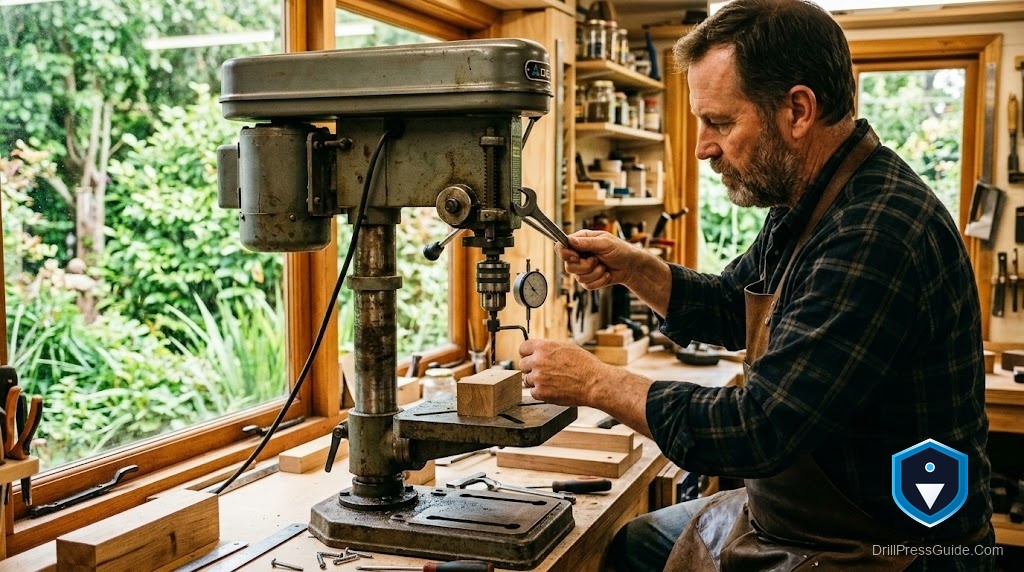
A wobbling bit is more than annoying. It drills oversized, ragged holes, chews up bits, and can be a sign of a problem that gets worse if you ignore it. The reassuring part is that most drill press wobble comes from a short list of causes, and you can find yours in a few minutes with nothing more than a careful eye and maybe a dial indicator. Here is how to track it down and fix it.
Fixing drill press wobble means finding which part is causing the runout, the bit, the chuck, the spindle, or the setup, and correcting or replacing it so the bit runs true. Wobble is not one problem; it is a symptom with several possible sources, and the trick is to isolate the cause instead of throwing parts at it. Work from the simplest and most common cause outward, and you will usually fix it fast.
Here is the direct answer, in the order you should check. First, the bit: a bent bit or one seated crooked in the chuck is the most common and easiest cause, so try a known-good bit seated properly before anything else. Second, the chuck grip: chips or an uneven seat in the jaws throw the bit off, so clean the jaws and re-seat the bit square. Third, the chuck itself: a worn chuck with worn jaws will never hold a bit true and may need replacing. Fourth, the chuck-to-spindle mounting: a dirty or damaged taper where the chuck mounts causes wobble, so clean it or reseat it. Fifth, the spindle and quill: worn bearings or excess quill play are the deeper causes. Check in that order and you will find most wobbles at step one or two.
Start with the bit and the setup
Before you suspect the machine, suspect the bit. A dropped bit can bend just enough to wobble, and a bit that is not pushed fully and squarely into the chuck jaws will run off-center. Swap in a bit you trust, seat it fully with the jaws gripping the straight part of the shank evenly, and tighten in all three chuck-key positions so the jaws close evenly. A surprising share of wobble complaints end right here.
While you are at it, make sure the wobble is real and not the eye playing tricks at speed. Lower the quill and spin the chuck by hand, watching the bit tip against a fixed reference. If it visibly swings, you have runout to chase. If you want a number, a dial indicator against the spindle or a precision rod tells you how much, with under about five thousandths of an inch being fine for general work and under two thousandths counting as precise.
Work outward to the chuck and spindle
If a good bit still wobbles, move to the chuck. Open the jaws fully and clean out chips and grit, since debris in the jaws throws off the grip. Re-seat a precision rod and check again. If the chuck still runs out, its jaws may be worn, and a replacement chuck is the cure. A quality keyed drill chuck restores a true grip, and a matching drill chuck with arbor covers the case where the mounting arbor is also worn or the wrong taper.
Next check where the chuck mounts to the spindle. Most chucks seat on a taper; if that taper is dirty, dinged, or not fully seated, the chuck runs out no matter how good it is. Remove the chuck, clean both taper surfaces until they are spotless, and reseat firmly. If wobble persists after all this, the cause is deeper, worn spindle bearings or excessive quill play, which is a bearing or quill service. The Occupational Safety and Health Administration’s guidance to unplug the machine before reaching into the chuck or spindle applies to every one of these checks.
Comparison: cleaning and reseating versus replacing parts
Cleaning and reseating the bit, jaws, and taper takes only a few minutes and fixes the large majority of wobbles, but it will not save a chuck whose jaws are genuinely worn out.
Replacing the chuck or arbor cures wobble that cleaning cannot, restoring a true grip, though it costs a part and a few minutes to swap.
My verdict: always work from the simplest fix outward. Clean and reseat first, because most wobble is a dirty taper or a badly seated bit. Only replace the chuck or arbor once you have proven the grip itself is worn, and only suspect bearings after everything upstream checks out true.
Conclusion
Drill press wobble is a runout hunt, and the order is everything: bit, chuck grip, chuck condition, taper mounting, then spindle and quill. Most wobbles fall out at a bent bit, a badly seated bit, or a dirty taper, all free to fix. Replace the chuck or arbor only when the grip is proven worn, and service bearings last. Chase it in order and you will have a true-running machine again quickly.
Key takeaways:
- Check in order: bit, chuck grip, chuck condition, chuck-to-spindle taper, then spindle and quill.
- Most wobble is a bent or badly seated bit, or a dirty mounting taper, all free to fix.
- Replace a worn chuck or arbor only after cleaning and reseating fail to fix the runout.
FAQ
Why does my drill press bit wobble? Most often a bent or badly seated bit, a dirty chuck, or a dirty chuck-to-spindle taper. Worn bearings are a deeper cause.
What should I check first? Swap in a known-good bit and seat it fully and squarely in clean chuck jaws.
How much runout is acceptable? Under about five thousandths of an inch is fine for general work; under two thousandths is precise.
How do I measure wobble? With a dial indicator against the spindle or a precision rod, or by eye against a fixed reference at low speed.
When should I replace the chuck? When a good bit still runs out after cleaning the jaws and taper, indicating worn chuck jaws.
Could the taper be the problem? Yes. A dirty or damaged taper where the chuck mounts causes wobble; clean both surfaces and reseat.
What if it still wobbles after all that? The cause is likely worn spindle bearings or quill play, which needs a bearing or quill service.
References
- Occupational Safety and Health Administration, Woodworking eTool: Drill Presses (osha.gov)
- Industrial Monitor Direct and machining references on acceptable spindle runout tolerances