How to Tap a Hole with a Drill Press, Step by Step
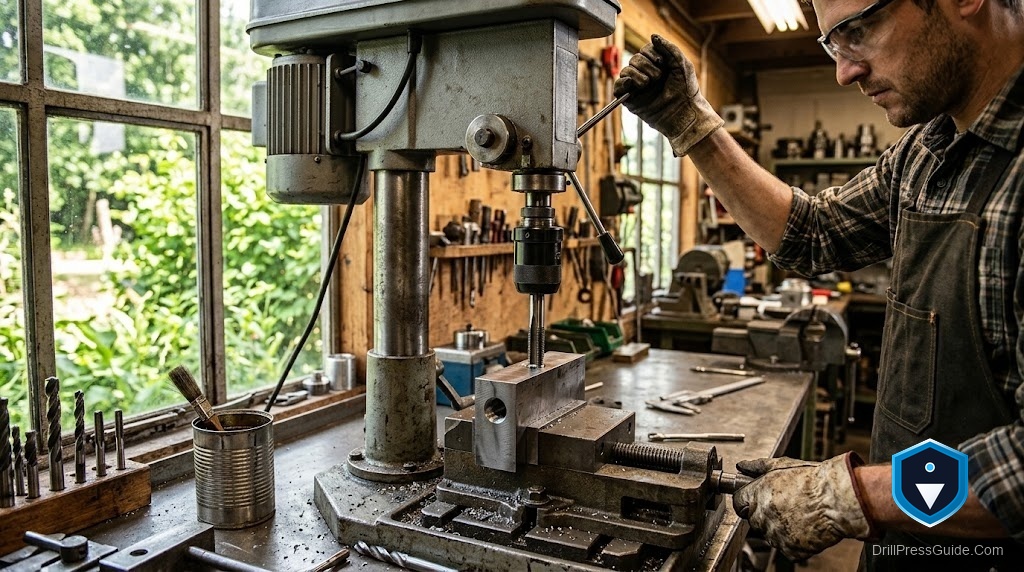
Stripped threads and snapped taps almost always come from one thing: a tap that started crooked. The drill press is the best tool most home shops own for fixing that, because it holds the tap perfectly square to the hole. The catch is that you do not tap under power the way you drill. Do it right and you will cut clean, straight threads every time. Do it wrong and you will fish a broken tap out of a good part.
Tapping a hole with a drill press means using the machine to keep a hand tap aligned straight with the hole while you turn the tap to cut threads, usually by hand rather than under motor power. The drill press supplies the one thing that matters most in tapping, perfect alignment between the tap and the hole, so the threads start square and stay square. The motor does not drive the tap in the safe methods; the spindle simply guides it.
Here is the direct answer, step by step. First, drill the correct tap-drill size for your thread, because the wrong starter hole is the top cause of bad threads. Second, with the power off, lower the tap into the hole and use the spindle to hold it square. The safe way to turn is by hand: fit the tap in a tap wrench and turn it while a center in the drill chuck presses down on the tap’s center hole to keep it aligned, or use a spring-loaded tap guide held in the chuck that keeps downward alignment while you turn the wrench. Third, turn forward about half a turn, then back a quarter turn to break the chip, and repeat, using cutting fluid throughout. Never run the motor to power-tap unless you have a true tapping head made for it. That hand-turned, spindle-guided method is what gives you straight threads without broken taps.
Start with the right hole
Threads are only as good as the tap-drill hole. Every tap has a matching drill size, and using it leaves the correct amount of material for the tap to cut. Too small and the tap binds and snaps; too large and the threads come out shallow and weak. Look up the tap-drill size for your thread and drill it on the same drill press, in the same setup, so the tap follows a hole that is already square to the spindle. That single habit prevents most tapping grief.
Deburr the top of the hole lightly so the tap starts clean, and clamp the work in a vise so it cannot spin. A workpiece that turns with the tap is both a ruined thread and a hazard at the point of operation.
Keep the tap square, turn it by hand
Alignment is the drill press’s gift to tapping. Two methods use it safely. In the first, you put a pointed center in the drill chuck and rest it in the center hole on top of the tap while you turn the tap with a tap wrench by hand; the center keeps the tap plumb as you feed the quill down gently to follow the thread. In the second, a spring-loaded tap guide chucks into the spindle and holds the tap aligned under light spring pressure while you turn the wrench, which keeps the tap square with less juggling. Either way, your hand turns the tap, not the motor.
Turn forward roughly half a turn, then reverse a quarter turn to snap the chip so it does not pack and jam. Use tapping fluid on metal to ease the cut and clear chips. Go gently; the tap tells you through the wrench when a chip is binding, and forcing through that feeling is how taps break.
When power tapping is fine, and when it is not
Straight power tapping by running the motor is risky on an ordinary drill press: there is no clean reverse under load, and a tap that bottoms out or binds will snap or spin the work. Only a dedicated tapping head, which reverses automatically when you lift, makes powered tapping safe. Without one, keep the power off and turn by hand. The Occupational Safety and Health Administration’s drill press guidance around clamped work and a controlled point of operation lines up with hand tapping, not with muscling a powered tap through a blind hole.
Comparison: center-guided hand tapping versus a tap guide
Center-guided hand tapping needs only a pointed center you likely own, and it holds the tap square well, but it takes two hands and some coordination to keep the center seated while you turn.
A spring-loaded tap guide holds alignment for you under spring pressure, freeing your attention for the wrench, though it is one more accessory to buy.
My verdict: for occasional tapping, the center-in-the-chuck method uses only a center you likely own and works. If you tap often or hate fishing out broken taps, a spring-loaded tap guide pays you back in straight threads and whole taps.
Conclusion
Tapping on a drill press is really about alignment, and the machine gives you that for free. Drill the right tap-drill hole, hold the tap square with a center or a tap guide, turn by hand with a forward-and-back rhythm, and keep it wet with cutting fluid. Skip the temptation to power-tap without a tapping head, and you will cut clean threads without the snap.
Key takeaways:
- Drill the correct tap-drill size first; the wrong hole causes most broken taps.
- Use the spindle to hold the tap square, but turn the tap by hand, not under motor power.
- Go forward a half turn, back a quarter to break the chip, with cutting fluid throughout.
FAQ
Can I tap a hole with a drill press? Yes, to hold the tap square while you turn it by hand. Do not power-tap without a dedicated tapping head.
Why not just run the motor? An ordinary drill press has no safe reverse under load, so a binding tap will snap or spin the work.
What hole size do I drill first? The tap-drill size that matches your thread. Using it leaves the right material for the tap to cut.
How do I keep the tap straight? Hold a center in the chuck against the tap’s center hole, or use a spring-loaded tap guide in the spindle.
Why turn forward then back? Reversing a quarter turn breaks the chip so it does not pack and jam the tap.
Do I need cutting fluid? On metal, yes. It eases the cut, improves the thread, and helps clear chips.
What is a tapping head? An accessory that reverses automatically when you lift the quill, which is what makes powered tapping safe.
References
- Occupational Safety and Health Administration, Woodworking eTool: Drill Presses (osha.gov)
- Machinery’s Handbook, Industrial Press, tap-drill sizes and tapping practice