How to Remove Drill Press Chuck Chicago Machinery: What to Check Before You Start
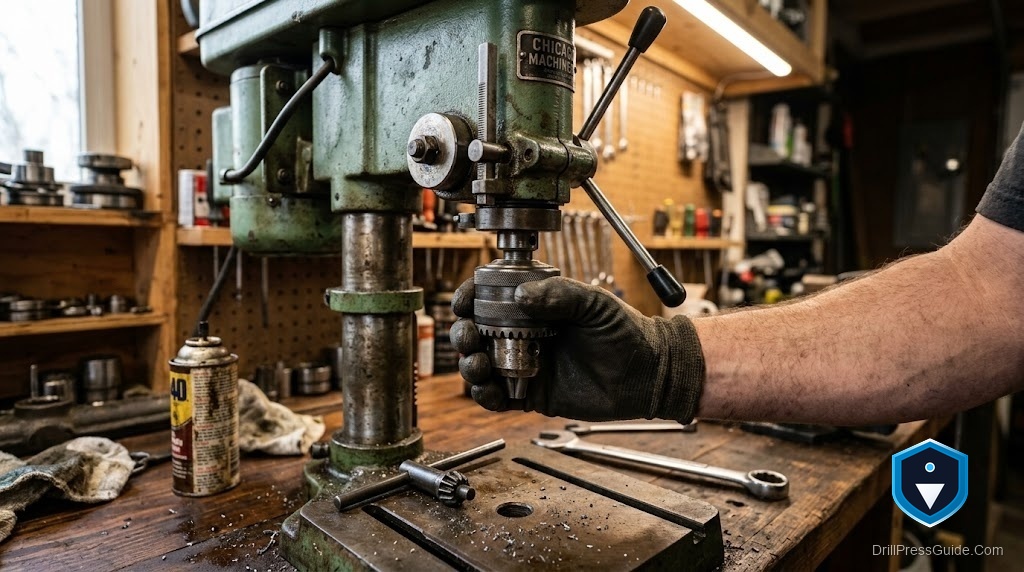
Chicago Machinery and Chicago Electric presses are common home-shop machines, and when the chuck needs to come off for a worn set of jaws or a keyless upgrade, the job trips people up only because they skip a couple of checks first. Knowing how to remove the drill press chuck on a Chicago Machinery press starts with confirming which taper you have and how to protect it, because that is what keeps the next chuck running true.
On these presses the chuck sits on an arbor whose Morse taper wedges into the spindle, and the chuck grips that arbor on a shorter Jacobs taper. Removing it means driving a drift or wedges into the spindle slot to press the arbor and chuck out, or pressing the chuck off its arbor if you are only changing the chuck.
Short answer: unplug the press, confirm whether you are removing the whole assembly or just the chuck, lower and lock the quill to expose the spindle slot, then drive a drift or wedges into the slot. Support the chuck and keep tools off the ground taper faces.
What to check before you start
- Which taper. Whole assembly means breaking the Morse taper at the spindle; chuck only means breaking the Jacobs taper at the arbor. The tool goes in a different place for each.
- Taper size. These presses commonly use an MT2 spindle with a JT33 chuck, but confirm yours before buying a replacement.
- Slot access. The spindle slot appears only when the quill is fully lowered and locked.
- Support plan. The chuck drops the instant the taper releases, so plan to catch it.
The tool that protects accuracy
A factory drift key works in the spindle slot if you have one. A drill chuck removal wedge set handles both the Morse and Jacobs joints and spreads force on the shoulders instead of the ground faces, which preserves the surfaces that center the chuck. It fits the JT33 and JT6 tapers on these presses.
The honest drawback: the chuck releases suddenly, so support it. Who should skip the wedges: anyone with a clean spindle slot and the correct factory drift.
Removing it, step by step
- Unplug the press.
- Decide: whole assembly, or just the chuck.
- For the assembly, lower and lock the quill to expose the spindle slot, then drive a drift or wedges into the slot.
- For the chuck alone, set wedges between the chuck and the arbor shoulder and press it off.
- Support the chuck so it lands soft, keeping tools off the taper faces.
- Wipe every taper dry and bright before refitting.
Run the checks, then break the taper
Removing a Chicago Machinery chuck goes smoothly once you confirm the taper, expose the slot, and plan to catch the chuck. Then a drift or wedges on the shoulders free it without harming the surfaces that keep it true.
Three takeaways:
- Confirm which taper you are breaking, and its size, before you start.
- Expose the spindle slot by fully lowering and locking the quill.
- Support the chuck and reseat on clean, dry tapers so it runs true.
FAQ
How is the chuck held on a Chicago Machinery drill press? By a Jacobs-taper grip on a Morse-taper arbor that wedges into the spindle, commonly MT2 and JT33. It is friction, not threads, so you break the taper to remove it.
How do I remove the chuck? Lower and lock the quill to expose the spindle slot, then drive a drift key or wedges into the slot to press the arbor and chuck out.
What chuck key size do these presses use? It varies by chuck; the size is stamped on the key and chuck body. Match that number, or switch to a keyless chuck to skip the key.
How do I remove just the chuck, not the arbor? Set wedges between the chuck and the arbor shoulder and press the chuck off, leaving the arbor seated in the spindle.
The taper will not release. What now? Soak the joint with penetrating oil, wait, and try again. A seized taper needs time, not more force.
Why does the new chuck wobble? Usually a dirty or nicked taper. Clean all mating surfaces, inspect the arbor, and reseat before checking runout.
References
- Harbor Freight, Chicago Electric drill press manuals and parts: https://www.harborfreight.com
- VintageMachinery.org, drill press chuck and taper documentation: http://vintagemachinery.org